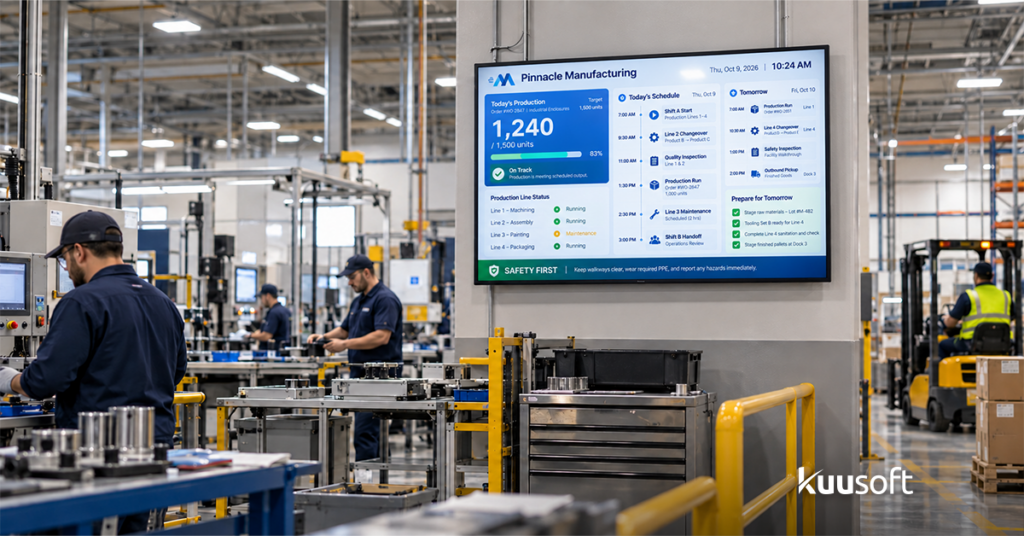
Safety and productivity on the factory floor depend on clear, real-time communication. When production schedules change, when hazards emerge, or when employees need instant updates, seconds matter. Traditional static signage can’t keep up. A printed notice taped to the wall doesn’t tell your team about a shift in quality standards, a new safety protocol, or a production milestone.
This is where manufacturing and warehouse digital signage makes the difference. It transforms how you communicate across your facility by replacing paper notices with dynamic, data-driven displays that connect directly to your production systems. The result: safer operations, more engaged employees, and measurable improvements in compliance and efficiency.
In this guide, we’ll explore how digital signage works in warehouses and manufacturing environments, the specific benefits it delivers, and how NexSigns makes implementation straightforward for industrial operations.
What is Warehouse & Manufacturing Digital Signage?
Warehouse and manufacturing digital signage refers to networked display systems designed specifically for industrial environments. Unlike retail digital signage, which prioritizes aesthetics and customer engagement, industrial signage prioritizes durability, real-time data integration, and safety compliance.
These systems consist of:
- Rugged displays built to withstand dust, moisture, temperature fluctuations, and physical impact.
Industrial-grade hardware designed for continuous operation in harsh conditions.
Real-time data integration that pulls live production metrics, inventory counts, and safety alerts from your systems.
Cloud-based content management for remote control across multiple locations and shift schedules.
Emergency override capabilities to broadcast urgent safety messages instantly.
Multi-location synchronization so corporate messaging reaches every facility at the same time.
Whether you manage a large distribution center, automotive plant, food processing facility, or manufacturing floor, digital signage becomes part of your operational infrastructure, not simply another communication tool.
Key Benefits of Digital Signage in Manufacturing & Warehouses
Warehouse and manufacturing digital signage refers to networked display systems designed specifically for industrial environments. Unlike retail digital signage, which prioritizes aesthetics and customer engagement, industrial signage prioritizes durability, real-time data integration, and safety compliance.
1. Safety Compliance & Hazard Communication
Manufacturing environments face strict regulatory requirements. OSHA, EPA, and industry-specific standards demand that safety information be visible, current, and accessible. Digital signage automates compliance by:
Displaying required safety data sheets and hazard information in real-time.
Showing incident reports and near-miss alerts to prevent repeat accidents.
Rotating safety tips and trainings based on daily operations.
Ensuring all displays show consistent, updated safety protocols across multiple facilities.
Creating audit trails that demonstrate regulatory compliance to inspectors.
A study by the National Safety Council found that facilities using digital safety communications reduced incident rates by up to 30% compared to those relying on static signage alone.
2. Real-Time Production KPIs & Operational Transparency
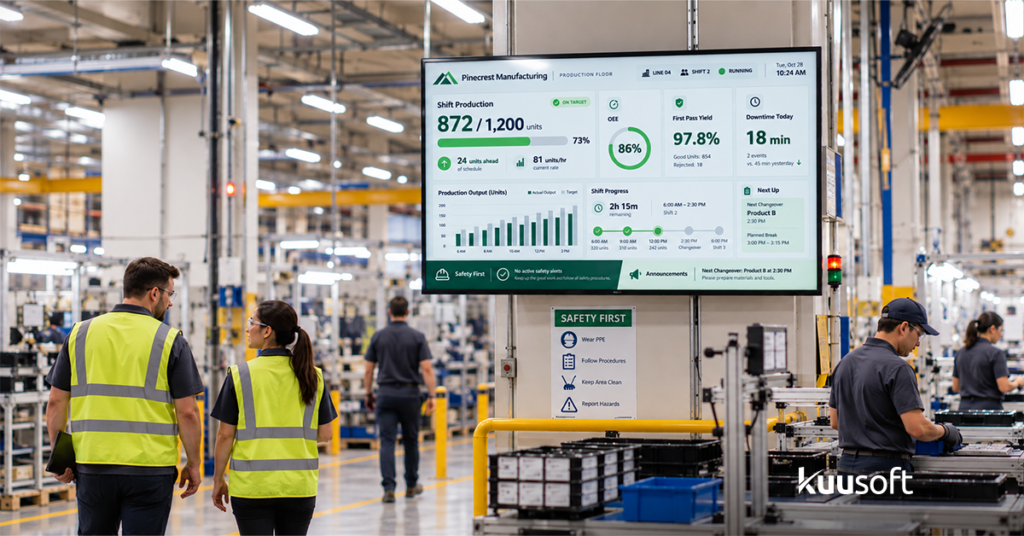
Manufacturing leadership depends on visibility into production performance. Digital signage brings key metrics directly to the floor:
Live production dashboards show current output, downtime, efficiency rates, and OEE (Overall Equipment Effectiveness).
Shift goals and progress keep teams aligned and motivated.
Quality metrics display defect rates, rework requirements, and corrective actions.
Inventory levels at loading docks and storage areas, preventing bottlenecks.
Machine status indicates which equipment is running, idle, or down for maintenance.
When employees see real-time production data on the floor, accountability increases. Workers understand how their performance contributes to facility-wide goals, and supervisors can quickly identify and address issues.
3. Employee Communication & Engagement
Warehouses and manufacturing plants employ hundreds, sometimes thousands, of people across multiple shifts. Keeping everyone informed is a challenge. Digital signage solves this by:
Broadcasting shift-specific announcements (start times, priorities, schedule changes).
Recognizing employee achievements, safety milestones, and team celebrations.
Sharing company news and updates that might otherwise be missed.
Displaying social content that builds culture and team cohesion.
Reducing reliance on individual emails or text messages that people might not see.
Engaged employees are more productive and more likely to follow safety protocols. Digital signage creates a shared information environment where nothing gets lost in translation.
4. Training & Knowledge Reinforcement
Continuous training is critical in manufacturing. Digital signage supports this by:
Rotating short training modules and safety refreshers throughout the day.
Displaying standard operating procedures (SOPs) at relevant work stations.
Showing equipment operation guides near machinery.
Providing onboarding content for new employees.
Recording training completion for compliance documentation.
Unlike a one-time training session, digital signage provides ongoing reinforcement. Employees see proper procedures repeatedly, improving retention and reducing errors.
5. Emergency Alerts & Rapid Response
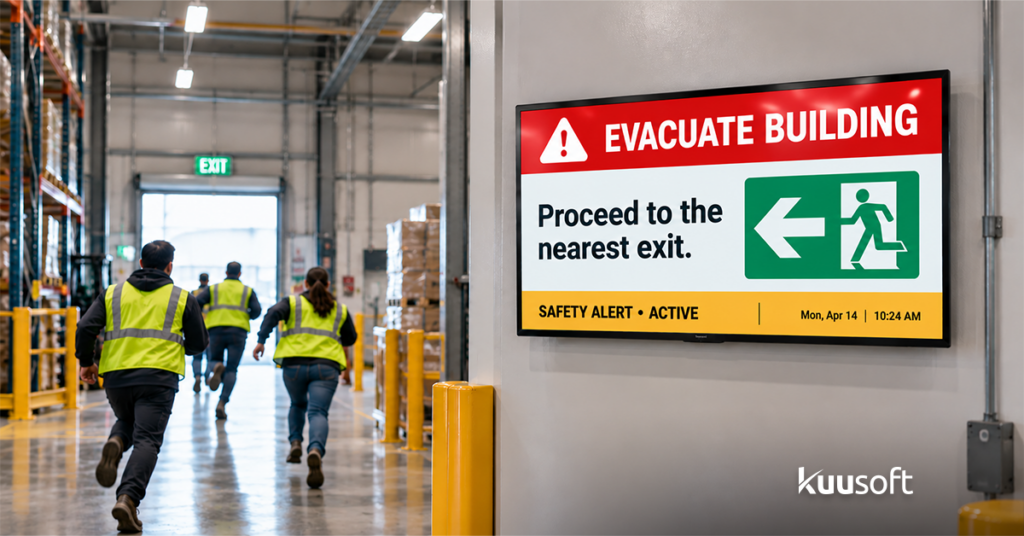
In a crisis, such as a chemical spill, equipment failure, or facility evacuation, every second counts. Digital signage enables:
One-touch emergency broadcasts that reach all screens simultaneously.
Escalated alerts that override regular content with critical safety messages.
Clear, visible instructions that employees see even in noisy, chaotic environments.
Multi-language support for diverse workforces.
Redundant communication so messages reach people who may miss PA announcements or sirens.
A manufacturing facility with 500 employees can broadcast an emergency evacuation message to every screen in seconds, ensuring maximum situational awareness.
Real-World Use Cases for Industrial Digital Signage
Production Floors
Manufacturing lines benefit from real-time dashboards showing line speed, defect counts, changeover status, and performance against targets. Operators can see if a line is running ahead or behind schedule and adjust accordingly. Supervisors monitor multiple lines from a central display.
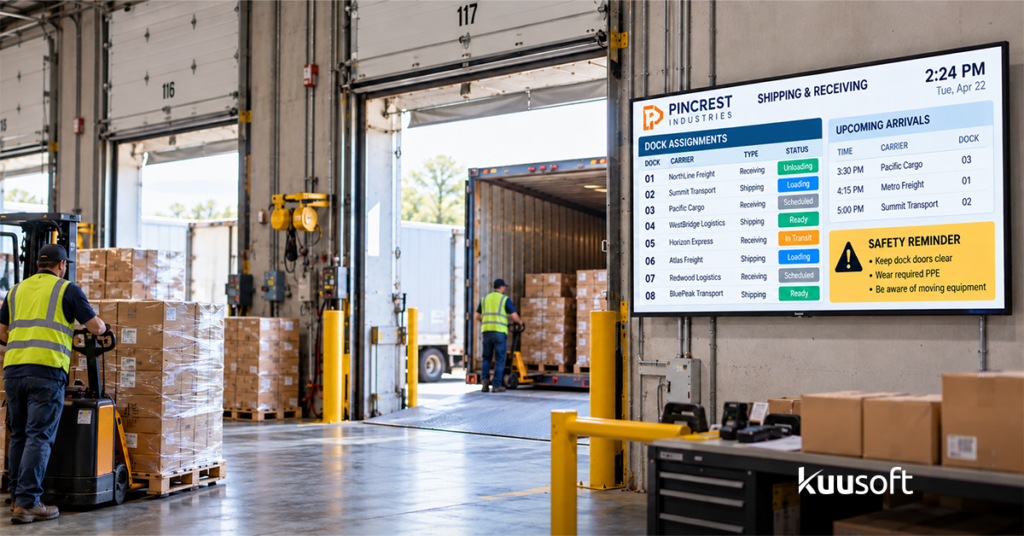
Loading Docks & Shipping Areas
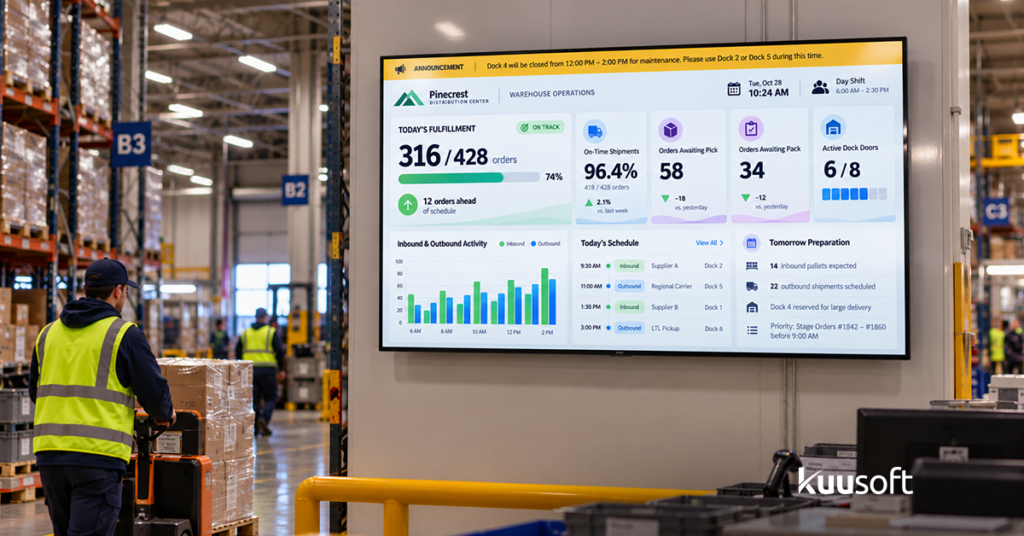
Distribution centers use displays to show incoming shipments, outgoing truck assignments, dock assignments, and performance metrics. This prevents missed shipments, reduces dwell time, and improves logistics efficiency.
Break Rooms & Common Areas
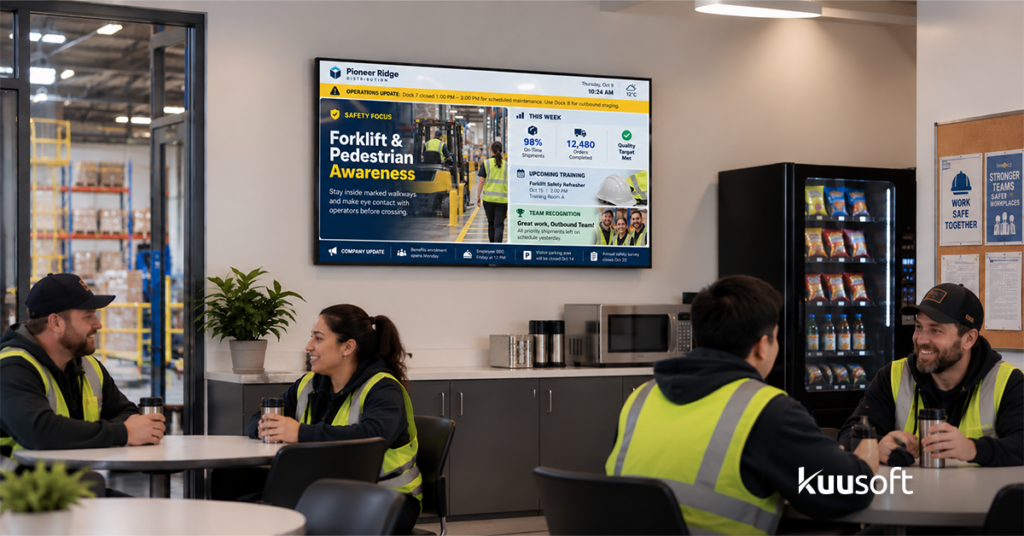
Break rooms are where employees gather during downtime. Displays here can share company announcements, safety tips, wellness information, and recognition content. It’s an ideal place to reinforce culture and celebrate wins
Facility Entrances & Visitor Centers
Visitor displays set the tone for your facility. They can show:
Current safety record (days without incident)
Safety messaging
Facility overview and emergency procedures
Company values and mission
Health & safety regulations
Quality Control Stations
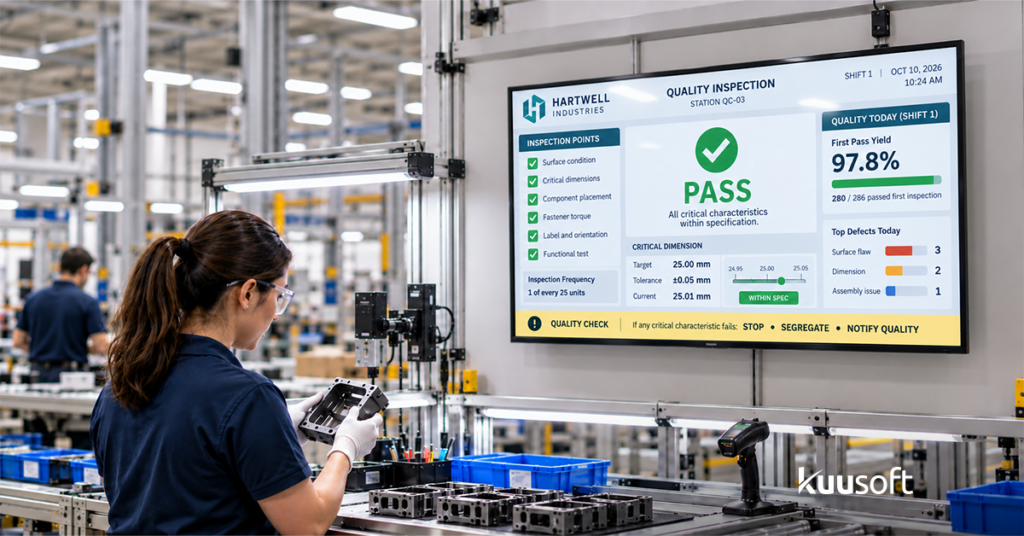
Quality teams need instant access to rejection data, trending issues, and corrective action status. Displays at QC stations can show real-time defect analysis and guide inspectors through updated standards.
Key Features to Look For in Manufacturing Digital Signage
When evaluating digital signage for your facility, prioritize these industrial-specific capabilities:
Rugged, Dust-Resistant Displays
Manufacturing environments are harsh. Displays must withstand:
Dust and particulate from production processes
Moisture in food processing or chemical facilities
Temperature extremes near ovens, freezers, or outdoor loading areas
Vibration from heavy machinery
Accidental impact
Look for industrial-grade displays with sealed enclosures, high brightness (for visibility in bright facilities), and wide operating temperature ranges.
Bright, Visible Displays
Warehouses and factories are often brightly lit or have variable lighting. Standard retail displays wash out in these environments. You need:
High nits (brightness) to remain visible under overhead lighting
Anti-glare coatings
Good contrast for visibility from across the floor
Look for industrial-grade displays with sealed enclosures, high brightness (for visibility in bright facilities), and wide operating temperature ranges.
Real-Time Data Integration
The power of industrial signage is its connection to your operational systems. Key integrations include:
ERP systems (SAP, Oracle) for production and inventory data
MES (Manufacturing Execution Systems) for real-time line metrics
Quality management systems for defect and trending data
Building management systems for facility status
HR/Scheduling systems for shift information
Custom APIs for proprietary systems
Emergency Override Capability
All displays must support instant override for safety messages. A critical alert should interrupt any content and reach all screens simultaneously, with no delays.
Multi-Location Management
If you operate multiple facilities, your signage system must:
Support hundreds or thousands of displays across locations
Allow corporate messaging to broadcast simultaneously across all sites
Enable local customization where each facility controls its own content
Provide consolidated reporting and compliance tracking
How NexSigns Powers Industrial Digital Signage
NexSigns, by Kuusoft, is purpose-built for warehouse and manufacturing environments. Here’s why facilities choose NexSigns:
Nano-PC Reliability
Our proprietary Nano-PC hardware is engineered for industrial demands:
Sealed design resistant to dust and moisture
Wide operating temperature range (-10°C to 60°C)
Fanless operation (less maintenance, more reliability)
Redundant power management for continuous uptime
Industrial-grade components rated for 24/7 operation
Unlike consumer-grade hardware repurposed for signage, the Nano-PC is built from the ground up for factories and warehouses.
Cloud CMS with Offline Capability
The NexSigns cloud-based content management system is designed for industrial operations:
Create and schedule content from anywhere, on any device.
Offline functionality ensures displays continue showing critical content even if cloud connectivity drops.
Template-based creation simplifies content updates for non-technical staff.
Drag-and-drop interface means no programming knowledge required.
Version control ensures you always know what’s displayed and when.
Real-Time Data Integration
NexSigns integrates seamlessly with the systems you already use:
Native connectors for major ERP platforms
REST API for custom integrations
Webhook support for event-triggered messages
Real-time refresh rates (not delayed reporting)
Data validation to ensure accuracy on displayed metrics
When your production system updates a KPI, NexSigns reflects that change on displays within seconds.
Multi-Location Management
Manage facilities across your enterprise from a single dashboard:
Global content distribution with local overrides
Per-facility scheduling and customization
Consolidated analytics and compliance reporting
Role-based access so facility managers control their locations
Bulk scheduling for corporate-wide campaigns
A company with 50 distribution centers can ensure brand consistency while allowing each to customize local announcements.
Emergency Override System
Safety is non-negotiable. NexSigns provides:
One-button emergency broadcast to all displays
Automatic escalation (overrides lower-priority content)
Customizable override messages for different emergency types
Compliance logging of all emergency broadcasts
Multi-language support for diverse facilities
Scheduling & Shift Management
Industrial operations run 24/7 across multiple shifts. NexSigns handles:
Shift-aware scheduling (different content for day, night, weekend shifts)
Automatic time zone synchronization across locations
Holiday and special event overrides
Recurring schedules that repeat automatically
One-time campaign scheduling for special announcements
Getting Started with NexSigns Today!
Ready to transform communication in your warehouse or manufacturing facility? NexSigns makes it simple. Get started today.


